
01
Finalize your design
Sizes, materials, finishes, and artwork are locked in. You review the proof carefully and approve when every detail matches your brief.
Shipping cartons rarely fail at the factory. They fail at the third forklift, the second conveyor drop, or the bottom of a stacked pallet. Heavy duty medical equipment boxes are engineered for that journey, so a patient monitor or infusion pump arrives calibrated, undamaged, and ready for clinical use.
The Packaging Masters builds double and triple wall shippers with custom foam, ESD protection, and strength ratings matched to your load. They protect everything from retail device cartons to bulk diagnostic kit shipments moving between warehouses.
What Makes Us Different?





From approval to doorstep — handled end to end.
Every order runs through four specialist teams — structural design, print, finishing, and dispatch — so your packaging keeps moving without bottlenecks, delays, or guesswork.
Sizes, materials, finishes, and artwork are locked in. You review the proof carefully and approve when every detail matches your brief.
Your job moves to print, cutting, lamination, and finishing. Our production team monitors color, registration, and structural accuracy.
Finished boxes are checked against the approved sample, counted, and securely packed to protect edges and print during transit.
Dispatch shares tracking details so your team can plan filling and launch dates. Your packaging arrives press-ready and production-ready.
Medical equipment is heavy, expensive, and often top-heavy. A standard single wall carton might hold the weight on a shelf, but it buckles when four more boxes are stacked on top in a truck. Corners crush, the unit shifts, and screens or sensor ports take the impact. One damaged ultrasound probe or monitor can cost more than an entire year of packaging.
Movement inside the box is the second killer. Loose fill settles during transit, leaving equipment free to slam into the walls with every bump. Electronics also face static discharge from ordinary plastic foam. Even master cases full of smaller cartons, such as our tuck end medicine boxes, need proper strength to avoid crushing the products inside.
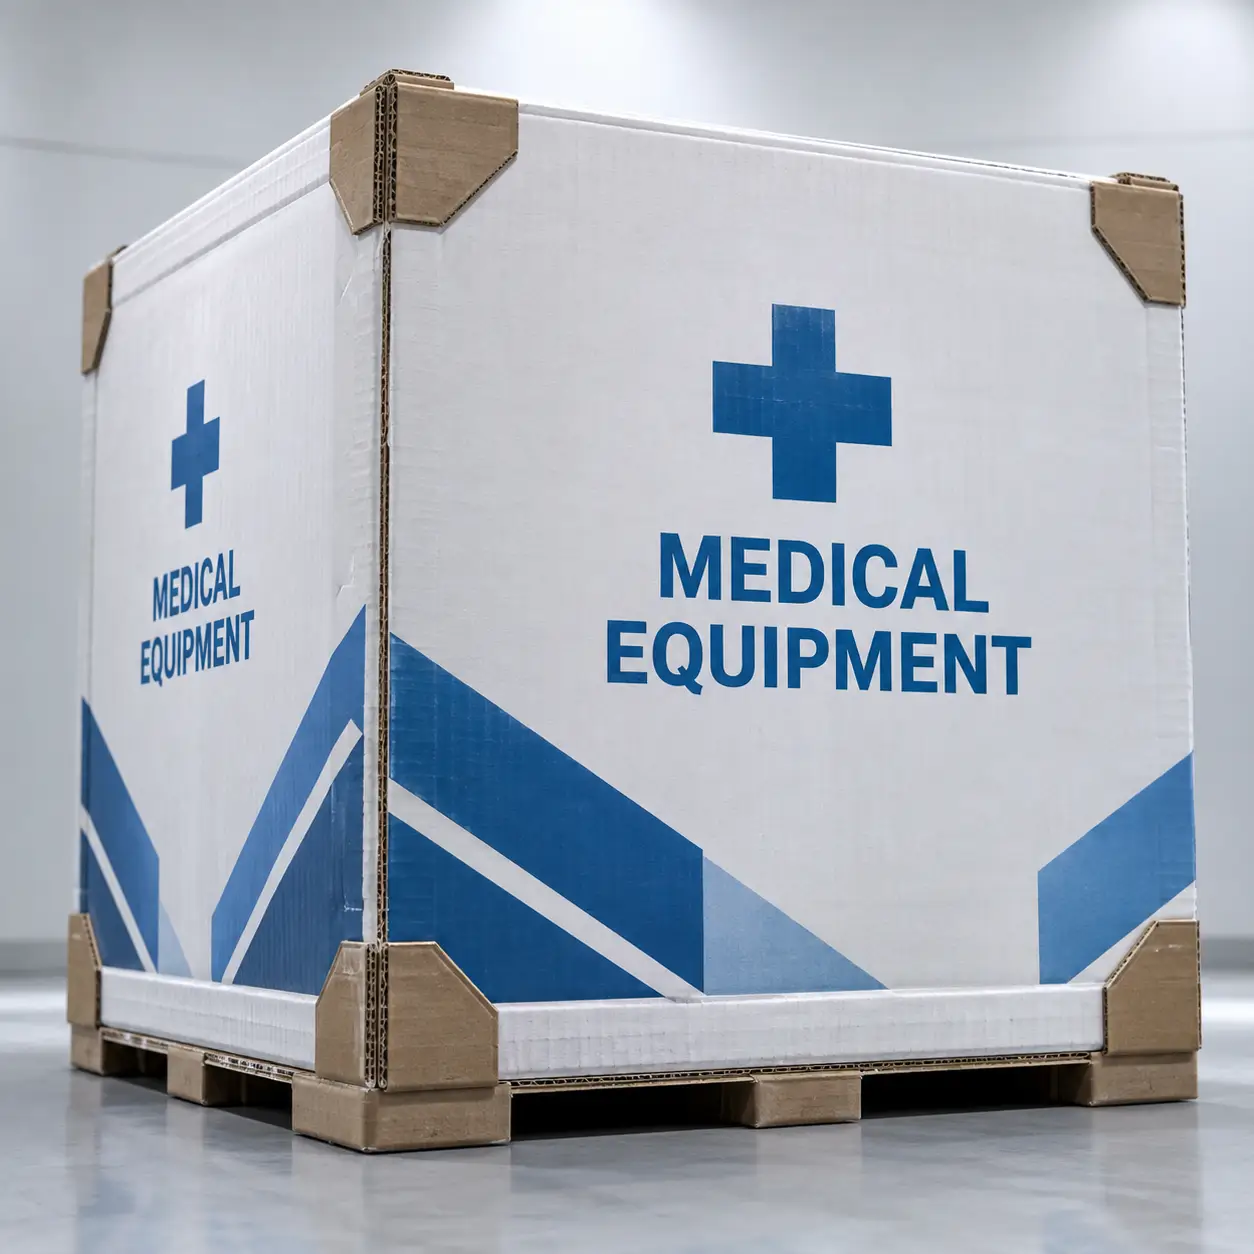
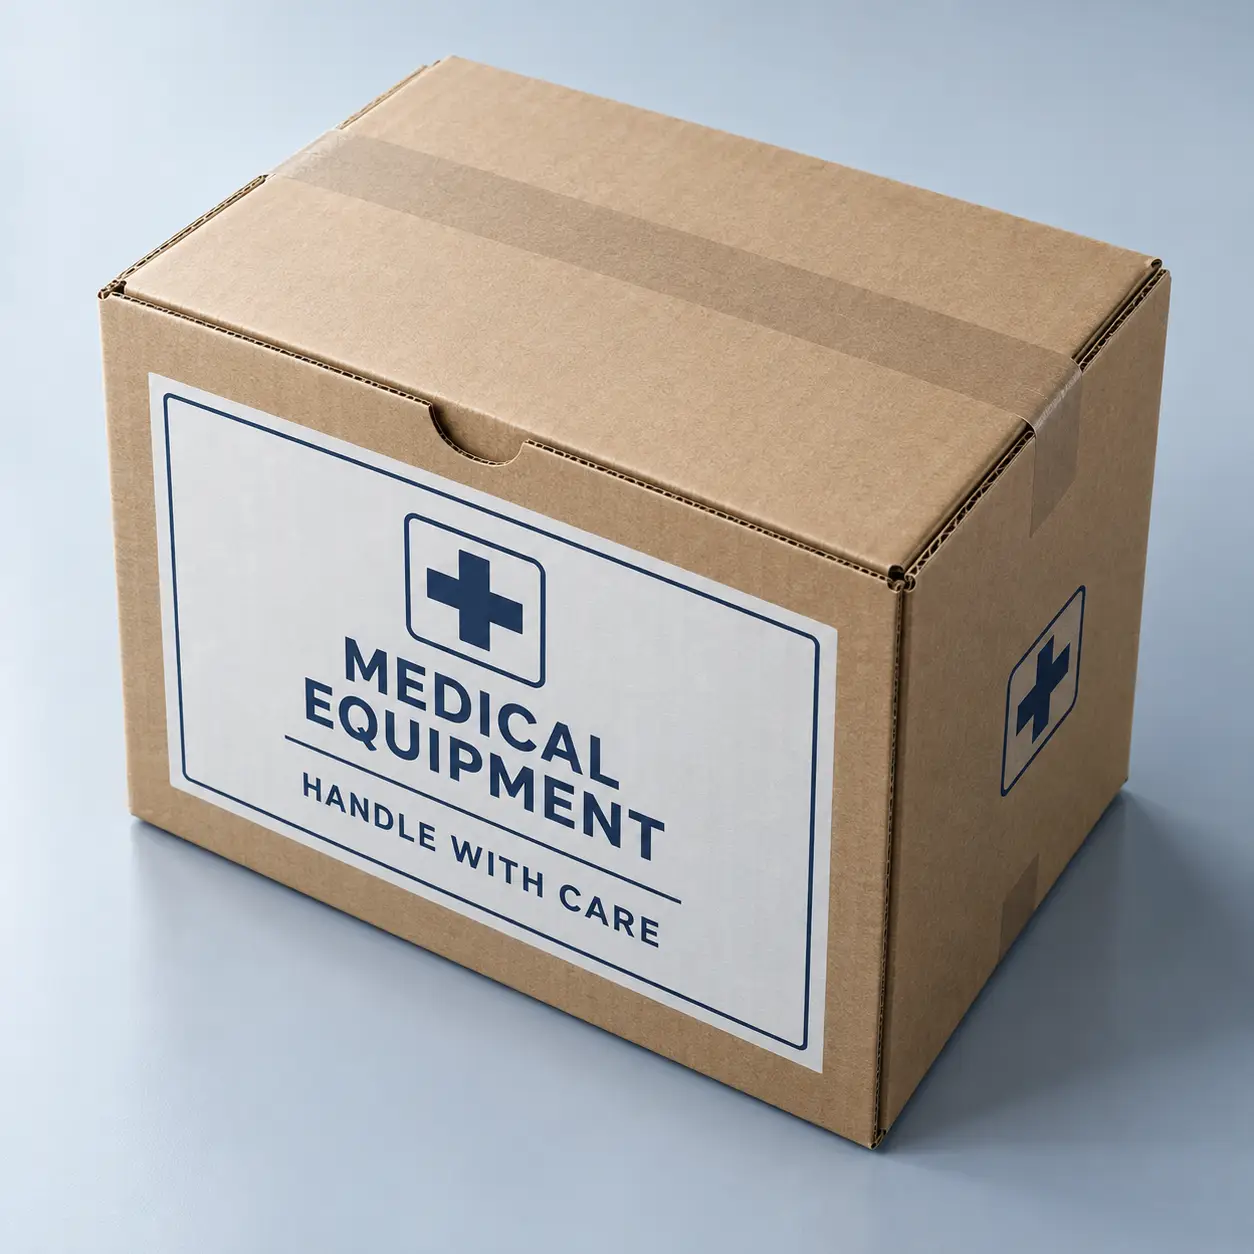
Well-engineered heavy duty medical equipment boxes combine the right flute and wall construction, custom-cut foam that holds the unit in place, and handling labels that guide carriers. Large trauma and Class B kits, like our first aid kit boxes, also benefit from sturdier outer shippers for distribution.
Most competitors promise strong boxes without saying how strong. Edge crush test ratings, or ECT, measure stacking strength and are the clearest way to compare corrugated options.
| Construction | Typical Rating | Common Use |
|---|---|---|
| Single wall | 32 to 44 ECT | Light devices and accessories |
| Double wall | 48 to 71 ECT | Monitors, pumps, and CPAP units |
| Triple wall | Heavy-duty grades | Large equipment and export shipments |
Foam choice matters as much as board. Polyethylene foam resists repeated impacts and moisture, polyurethane foam cushions delicate parts softly, and anti-static foam protects circuit boards and sensors. Many device manufacturers validate their packaging using ISTA test procedures that simulate drops, vibration, and compression. Corrugated board is widely recyclable, which we explain further in our eco friendly pharma cartons. We recommend the right combination based on your equipment weight, fragility, and shipping method, then confirm it with physical samples before production.
Device manufacturers ship patient monitors, infusion pumps, and diagnostic analyzers to hospitals worldwide. Distributors move pallets of mixed medical supplies between regional warehouses. Biomedical repair centers send equipment back and forth for servicing, so reusable shippers with replaceable foam save money over many trips. Home medical suppliers deliver CPAP machines, oxygen concentrator accessories, and mobility parts directly to patients.
Clinical research depots also need robust outer shippers for study supplies, alongside formats like our clinical trial packaging. Hazardous materials, lithium batteries, and temperature-sensitive products may require special packaging and markings, so confirm carrier rules with your logistics or compliance team.
Tell us your equipment dimensions, weight, and shipping method. We will recommend board grade, foam design, and closure, then send a structural proof within 24 hours. Request your quote today and ship heavy duty medical equipment boxes that arrive in one piece every time.
Start Your Quote
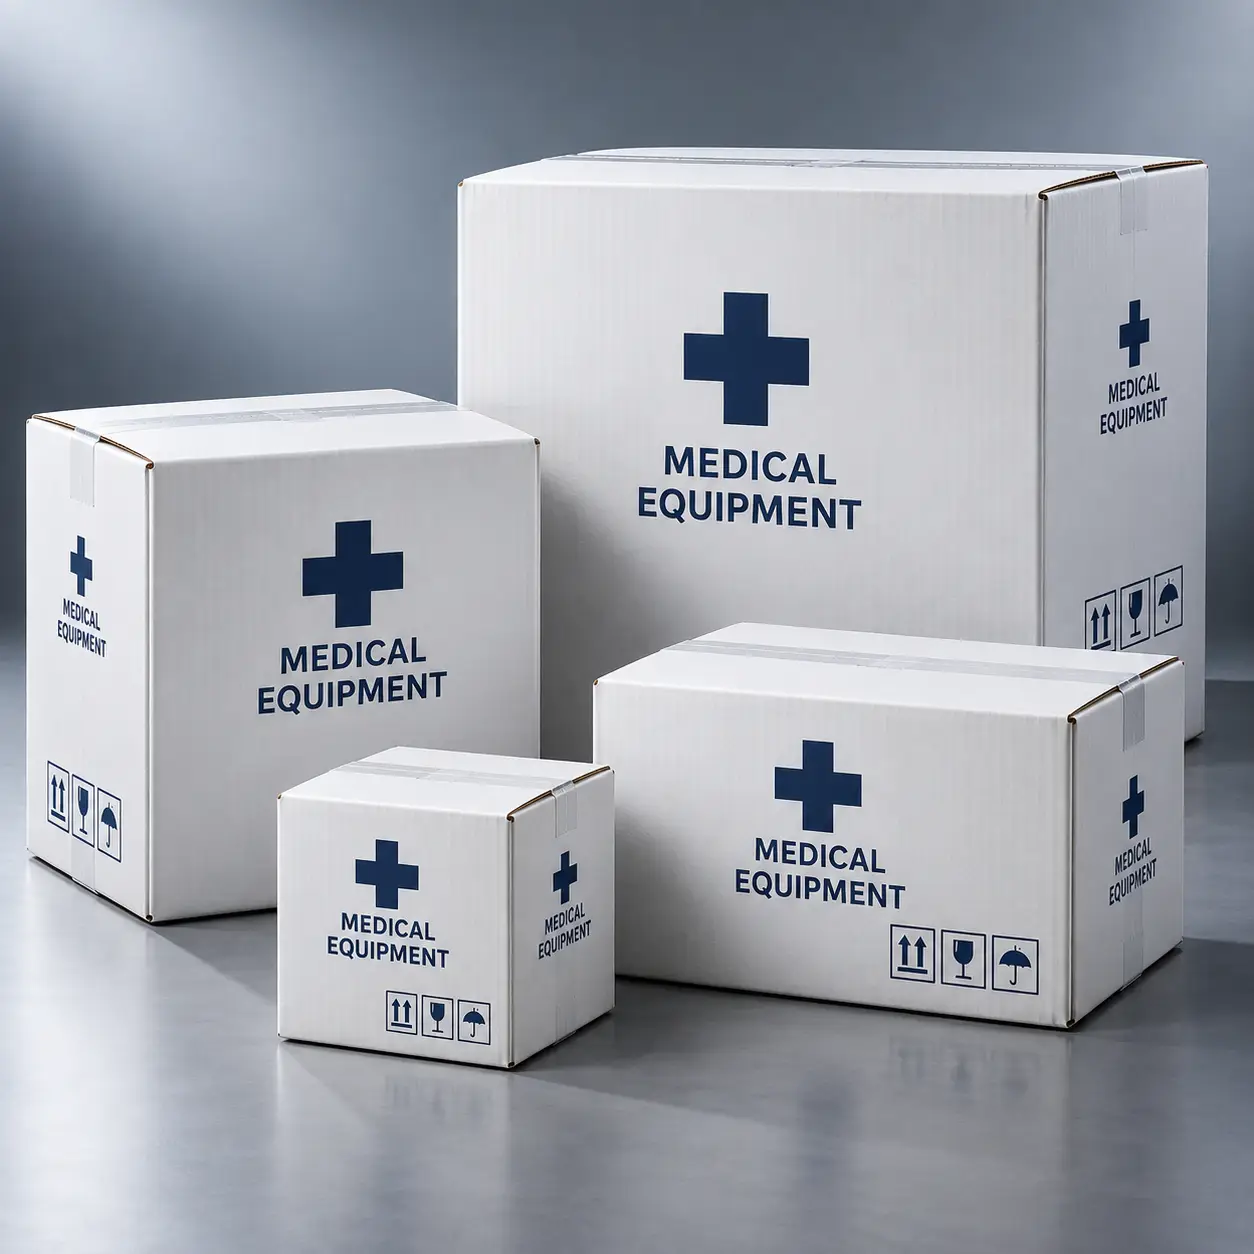
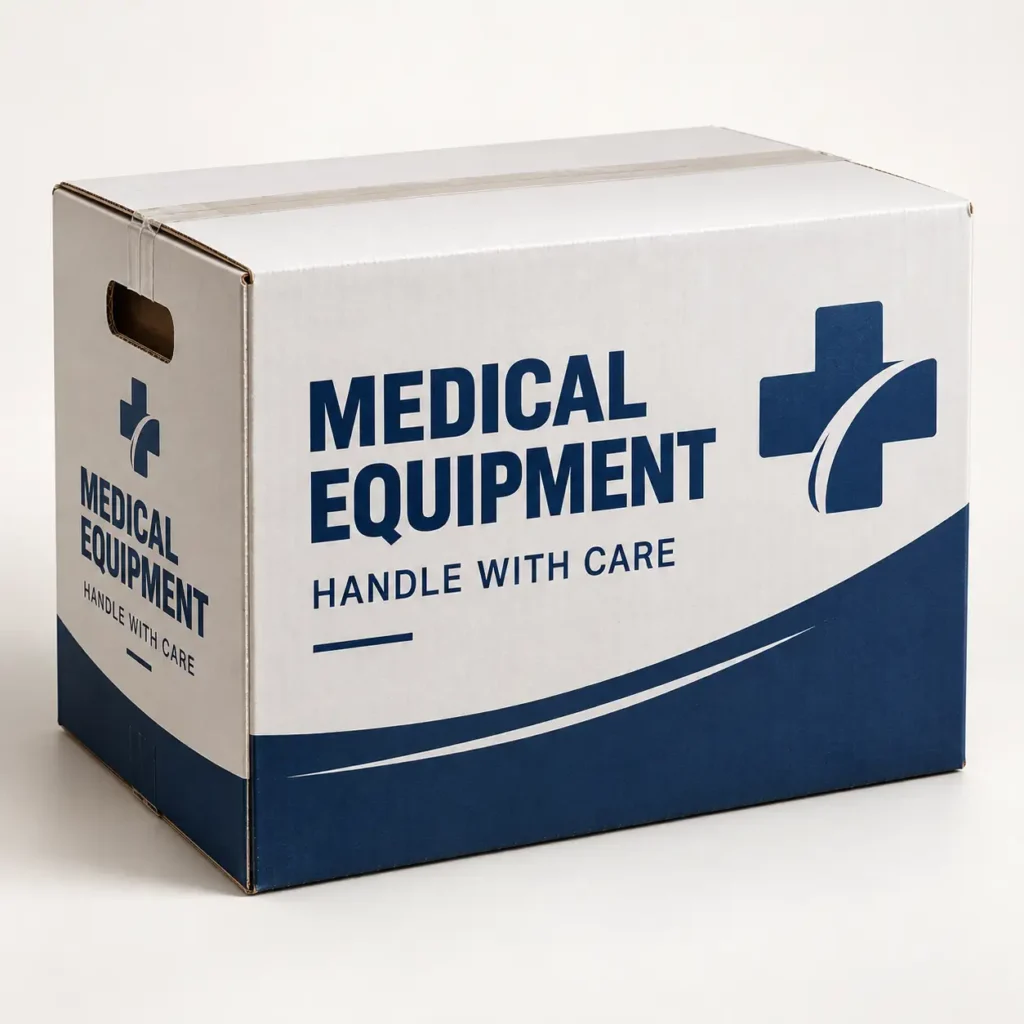
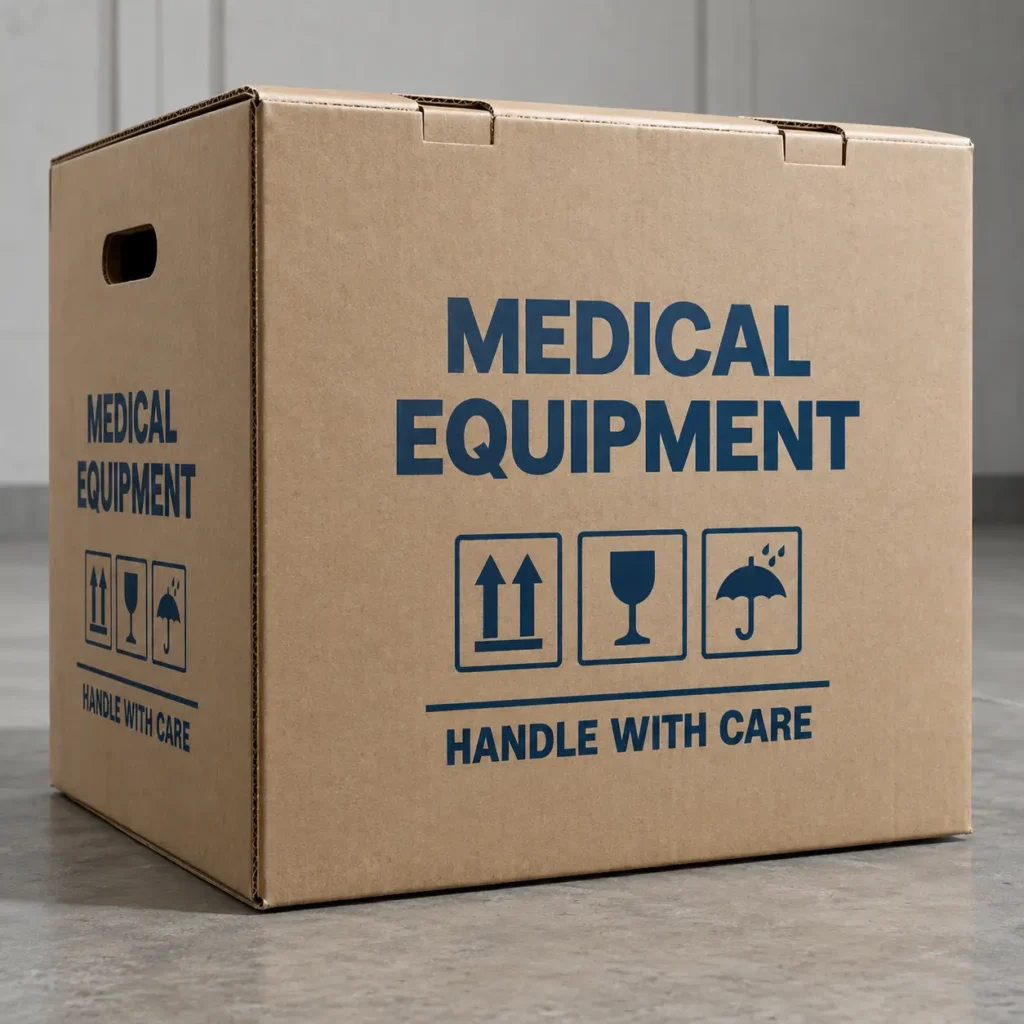
Clear handling symbols such as this side up, fragile, and keep dry help carriers treat your shipment properly. Printing model numbers, serial number windows, and barcode labels on the outer box speeds receiving at hospitals and distribution centers. Shock and tilt indicators can show whether a shipment was mishandled before it arrived.
High-value equipment also needs security. Printed security tape or tamper-evident labels, similar to our tamper-evident pharma packaging, show if a box was opened in transit. Hand holes make heavy boxes easier and safer to lift, and reinforced bottoms prevent sagging when pallets are moved.
Every order of heavy duty medical equipment boxes includes free design support, custom sizes, and quality checks on board grade, foam fit, and print accuracy. Request a free sample from The Packaging Masters, pack your real equipment, and run a simple drop test before approving production.
Heavy duty medical equipment boxes usually use double wall corrugated around 48 ECT or higher for monitors and pumps, and triple wall for large or export equipment. The right rating depends on weight, stacking height, and shipping method, so we recommend a grade after reviewing your equipment details.
Anti-static polyethylene foam is a common choice because it resists repeated impacts and reduces static discharge risk. Polyurethane foam suits very delicate parts that need softer cushioning. We cut foam to the exact contours of your device so it cannot shift during transit.
Yes. Veterinary clinics and animal hospitals use many of the same monitors, scales, and diagnostic units as human hospitals. Our veterinary medicine boxes cover smaller animal health products, while we design heavier corrugated shippers around your specific equipment dimensions, weight, and shipping routes.
Yes. Bulk tubs and canisters are heavy and need sturdy, well-sized master cases with dividers. Our protein powder packaging boxes show retail cartons, and we design corrugated shippers that protect them through busy warehouses, parcel networks, and retail distribution centers.
Yes. Pre-filled displays need an outer shipper so they arrive clean and undamaged. Our counter display pharma boxes explain display formats, and we size the outer carton to hold the display snugly with corner protection, clear opening instructions, and easy-tear access.
For repair and rental programs, often yes. Reusable shippers with heavier board and replaceable foam can make many round trips, lowering cost per shipment and reducing waste. We design them with reinforced handles, durable closures, and labels that are easy to update.
Custom heavy duty shippers start around $2.50 per unit at volume. Pricing depends on size, wall construction, foam type, printing, and quantity. Complex foam cradles and printing add some cost. We send detailed wholesale quotes within 24 hours, with lower pricing at larger quantities.
Corrugated shippers with foam inserts usually ship in about 12 to 18 business days after structural approval. Complex foam designs or special board grades may take longer. Rush options are available, and we confirm your full timeline in the quote, including freight delivery.
Instead of generic stock boxes, every project starts with your product, your goals, and your customer experience — so the packaging protects in transit and still feels premium in hand.
Built to your product, not pulled from a shelf of ready-made sizes.
Strong structures, neat edges, and finishes that actually sell.
Businesses and individuals can order — start with a small run and scale when you’re ready.
4–5 business days production after proof approval — you always know what’s next.
Copyright © 2026 thepackagingmasters.com All rights reserved.